Alright, let’s cut to the chase—if you’re running a horizontal boring mill CNC and regularly dealing with heavy workpieces, you know the nightmare all too well. Last month, a guy from a heavy equipment manufacturing shop hit me up panicking because he’d been scrapping 2-ton steel castings left and right, his machine was grinding through tooling like it was butter, and he was scared his boring mill was gonna take a permanent hit. Sound familiar? Let’s walk through the exact steps we walk our customers through to fix this stuff, no fluff, no jargon that makes your head spin. Horizontal Boring Mill CNC
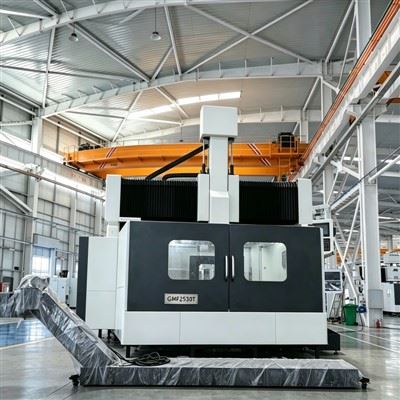
First off, let’s get one thing straight: heavy workpieces don’t have to be a disaster—you just can’t treat ’em like you’re milling a tiny aluminum block for a drone part. I see so many shops skip the prep work and jump straight to slapping the part on and cranking up the spindle speed, and that’s where everything goes wrong. Let’s start with the single biggest mistake I see all the time: fixturing like you’re working light parts. When you’re hauling around stuff that weighs 1,500 lbs or more, gravity is your enemy, and if your fixtures aren’t locked down tight, that part’s gonna shift mid-cut, not just ruining the finish but possibly bending your boring bar or even damaging the machine’s spindle. Wait, and don’t get me started on when guys just use regular clamps for this—no, you need heavy-duty, torque-rated clamps, not the cheap ones you picked up at the hardware store for a weekend project. We sell our customers rated pull studs too, because standard pull studs can’t handle the vibration from a 1,000-lb part bouncing around during a deep cut. Oh, and double-check every clamp before you hit “go” — once, a customer of ours almost sent a part through the side of the machine because he skipped the second check. Cost him 3 days of downtime, and that’s 3 days he couldn’t run other parts. Don’t be that guy.
Next up: workpiece setup. A lot of folks think “well, it’s heavy, so it’s stable” — no. A 3-ton casting that’s sitting on a flat plate might look stable, but if there’s even a tiny bit of debris under one edge, it’s tilting ever so slightly, and your boring operations are gonna be off by thousandths of an inch. For big parts, we always tell customers to use a dial indicator to truen the part after they clamp it, not before. And if you’re dealing with a super irregular shape? Use custom soft jaws or a custom fixture plate that’s been machined to match the part’s base. I know custom fixtures cost a little, but compare that to the cost of scrapping a $10,000 part. It’s a no-brainer. Also, make sure your machine’s table is rated for the total load — not just the workpiece, but the fixture, the tools, everything. Our horizontal boring mills have table load ratings that are clearly labeled, but I still get calls from guys using a machine that’s rated for 5 tons for a 6-ton part. That’s a ticking time bomb, plain and simple.
Then comes the cutting parameters, and this is where 90% of the heavy workpiece issues happen. I can’t tell you how many times I see a program that works for small parts run on a big, heavy one, and suddenly the spindle’s straining, the chips are wrong, and the tool’s breaking before the first pass is even done. First, slow down the spindle speed — way down. Heavy workpieces need more torque, not higher RPM. Our horizontal boring mills have variable torque settings, so you can bump up the torque output for thick steel or cast iron, which is a game-changer. If you’re running at too high a RPM, the tool’s just rubbing instead of cutting, generating tons of heat, and wearing out fast. I usually tell customers to start at 150-200 SFM for steel, adjust based on the material, and go from there. Then the feed rate: keep it low, too. Deep cuts, not fast shallow ones. A lot of guys think faster feed = faster part, but when you’re dealing with heavy stock, faster feed means more stress on the tool and the machine. We advise taking lighter radial cuts and deeper axial cuts — it’s way more efficient and way less likely to cause vibration. Vibration is the #1 enemy of heavy machining, by the way. It’s what causes those terrible chatter marks on the part, it breaks tools, and it wears out the machine’s ways. To fight vibration, make sure your boring bar is as short as possible — extend it only as much as you need to reach the feature you’re boring. A long, skinny boring bar is just asking for flex. Also, use a heavy-duty boring bar, not a standard one. Our customers swear by the carbide-tipped ones for big parts because they hold up so much better under pressure.
Wait, let’s not forget chip control. When you’re cutting heavy material, you get big, thick chips — and if those chips get stuck between the part and the fixture, or in the machine’s ways, they can scratch the part, damage the machine, or even cause the tool to break. You need to clear chips as you go, but don’t use a high-pressure coolant that blasts chips everywhere — that can shift a heavy workpiece. Instead, use a medium-pressure coolant aimed right at the cutting zone, and make sure your machine’s chip conveyor is working properly. We even have customers add small magnetic sweepers around the machine table to pick up any tiny metal shavings that get left behind. It’s a simple step that saves a lot of headaches.
Now, machine maintenance — you can’t ignore this when you’re running heavy workpieces. Our horizontal boring mills are built tough, but they still need regular upkeep to handle constant heavy loads. You have to check the ways and the gibs regularly — if the gibs are too loose, the table will shift and cause inaccuracies, and if they’re too tight, you’ll be putting extra strain on the motor. Also, keep the spindle lubricated — heavy cuts mean more heat, and a dry spindle is gonna overheat and fail fast. I always tell customers to follow the maintenance schedule we give them, not wait until something breaks. One of our regulars skipped the quarterly lubrication for his spindle and ended up with a $12,000 spindle replacement. That’s way more than the cost of doing the maintenance on time.
And here’s a pro tip I only share with our best customers: test cuts. Before you run your final program on a $20,000 workpiece, run a test cut on a scrap piece of the same material, same thickness, same shape. It takes an extra 30 minutes, but it saves you from scrapping a part that cost weeks to make. We usually recommend running the test cut at 50% of your desired parameters first, make sure everything’s stable, then bump it up. Last year, a customer of ours was machining a nuclear component that had super tight tolerances, and the test cut caught a minor fixturing issue that would’ve cost him over $500k if he’d missed it. No joke — that’s how important test cuts are.
Wait, what about when you’re boring a really deep hole, like 2 feet deep or more? That’s a whole different beast. Deep hole boring with a heavy workpiece means the boring bar is longer, so more flex, more vibration. We tell customers to use peck boring, not continuous boring. Pecking lets you clear chips from the hole, reduces heat, and prevents the bar from binding. Also, use a chip breaker insert on your tool — it breaks those big long chips into small ones that are easier to clear. I see a lot of guys skip the chip breaker, and they end up with a huge chip wrapped around the boring bar, which can yank the tool right out of the spindle and into the part.
Now, let’s address the elephant in the room: if you’re still having problems, maybe your machine isn’t the right fit. A lot of shops buy used horizontal boring mills because they’re cheap, but they don’t check the load capacity or torque rating. Our machines are purpose-built for heavy workpieces — we design the spindles with extra torque, the tables with extra load capacity, and the frames to withstand the constant vibration and stress. I don’t sell a machine to a customer if I think it’s gonna struggle with their workload, even if they try to talk me into it. It’s better to have a customer run parts without issues than to have them call me complaining about broken tools and scrapped parts.

At the end of the day, handling heavy workpieces on a horizontal boring mill CNC isn’t rocket science — it’s about paying attention to the details. Fixture right, set the part right, adjust your cutting parameters, maintain your machine, and don’t skip the test cuts. If you’re still running into issues, or if you’re in the market for a horizontal boring mill that’s built to handle heavy stuff, hit us up to talk through your needs. We don’t do one-size-fits-all solutions — we work with you to figure out exactly what your shop needs to get those big parts done without the headache.
Moving Beam Gantry References
- Machining Data Handbook, 5th Edition, Society of Manufacturing Engineers
- Horvath, J., "Heavy Workpiece Machining: Best Practices for Horizontal Boring Mills," Journal of Manufacturing Processes, Vol. 42, 2020, pp. 112-119
- Vibration Control in Machining Operations, American Machine Tool Distributors’ Association, 2019
5Axis (Shandong) CNC Equipment Co., Ltd.
As one of the most professional horizontal boring mill CNC manufacturers and suppliers in China, we also accept customized orders. Please feel free to buy cheap horizontal boring mill CNC for sale here from our factory. For price consultation, contact us.
Address: No.2000, Beixin West Road, Jinghe Street, Tengzhou City, Zaozhuang City, Shandong Province
E-mail: summer@good5axis.com
WebSite: https://www.china5axis.com/
