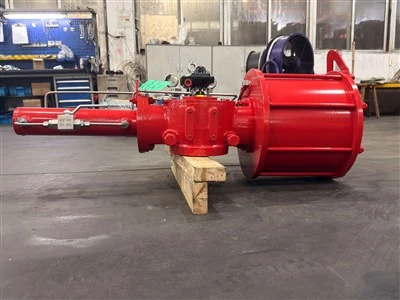
If you’ve ever stood next to a large, moving valve assembly in a refinery, power plant, or water treatment facility, chances are you’ve seen a Scotch Yoke Actuator in action. These workhorse devices convert rotary motion into linear force (or vice versa) to open and control heavy process valves, and they’re engineered to run nonstop—often in harsh environments where temperature swings, vibration, and constant pressure demand reliability. As a Scotch Yoke Actuator supplier, I’ve spent years working with plant maintenance teams, reliability engineers, and process operators, and one question comes up more than any other: “What sensors do I need to install on these things to keep them running, avoid unplanned downtime, and extend their lifespan?” Scotch Yoke Actuator

Too often, I see facilities either under-sensor their actuators (leading to surprise failures that cost thousands in lost production) or over-sensor them (wasting money on data that never gets used). The sweet spot is combining industry-standard sensors with real-world operational needs, tailored to the unique demands of Scotch Yoke design. Unlike rack-and-pinion actuators, Scotch Yokes use a sliding yoke and connecting rod to transfer force, which means they have distinct moving parts and failure points that need specific monitoring. Let’s break down the sensors we recommend, why they matter, and how we’ve seen them pay off for our customers.
First, start with the most critical: position sensors. The entire purpose of a Scotch Yoke Actuator is to move a valve to a precise open or closed position, and even a 1% deviation can throw off a process line, cause overpressure, or leave a valve partially open leading to erosion. There are three main types of position sensors we regularly specify, each suited to different use cases. For hazardous areas (think chemical plants with explosive vapors), we use non-contact inductive position sensors. These have no moving parts to wear out, so they’re ideal for extreme temperatures (-40°F to 185°F, or even higher with special enclosures) and avoid the risk of sparking that comes with contact sensors. For applications where ultra-precision matters—like a steam turbine bypass valve that needs to adjust flow in increments of 0.5%—linear variable differential transformers (LVDTs) are the gold standard. LVDTs measure displacement with micron-level accuracy, and they work well for the long stroke lengths common in Scotch Yoke actuators (some are 12 inches or more, which strains other sensor types). The third option is rotary encoders, which we often pair with smaller Scotch Yoke actuators or when retrofitting existing equipment. Rotaries mount directly to the actuator’s output shaft, are easy to install, and provide consistent position data for valve control systems. Last year, we worked with a Midwest power plant that switched from a cheap contact position sensor to an inductive sensor on 16 of their main steam isolation valve actuators. Within six months, they caught a worn yoke bushing that was causing 2 degrees of position error—something they would have missed until a scheduled shutdown. That early detection saved them $120,000 in lost generation from an unplanned outage.
Next, load and force sensors. Scotch Yoke actuators generate massive force to move heavy valves—some large units output over 100,000 lbf—but that force also puts stress on internal components: the yoke, connecting rod, bearings, and valve stem. Monitoring force isn’t just for troubleshooting; it’s a window into how hard the actuator is working, which can reveal problems before they cause breakdown. The most common place to mount a load sensor is between the actuator’s connecting rod and the valve stem. This spot gives a direct measurement of the force being transferred to the valve, so if the sensor reads lower than expected during a full valve stroke, that tells us something is resisting the movement—like a corroded valve stem, a stuck disc, or even a buildup of debris in the valve body. For high-cycle actuators (those moving more than 1,000 times a year), we also recommend mounting strain gauges on the yoke itself. Strain gauges are thin, durable sensors that measure small deformations in the metal yoke as force is applied, and they can detect fatigue cracks that form over time from repeated stress. A food and beverage processing plant we supply was struggling with frequent valve seat failures on their high-pressure product transfer lines. After installing load sensors, they noticed that one actuator was generating 15% more force than the others every time it moved the discharge valve. Tearing down the valve, they found a misaligned seat that was causing uneven pressure—had they ignored the force data, the seat would have failed and contaminated a batch of product, costing an estimated $80,000 in product and cleanup.
Vibration sensors are non-negotiable for any rotating or reciprocating equipment, and Scotch Yokes are no exception. While they’re not the same as centrifugal pumps or motors that have high-speed rotating shafts, Scotch Yokes have several reciprocating parts (the yoke, the sliding pin, the connecting rod) that generate vibration patterns that change as wear or faults develop. We use two types of vibration sensors: accelerometers for high-frequency vibration (1,000 to 10,000 Hz) that indicate bearing wear or gear tooth damage, and proximity sensors for low-frequency vibration (10 to 1,000 Hz) that detect shaft misalignment or loose mounting bolts. The key here is setting baseline vibration levels for each specific actuator—no two sites have identical operating conditions, so generic alarm thresholds don’t work. For example, an actuator operating in a cold climate will have slightly higher baseline vibration than one in a temperate climate, because lubricants are thicker and moving parts experience more friction. We work with our customers to build custom baselines when we install their actuators, so when vibration exceeds the threshold, it’s a clear sign of a problem. Last year, a water treatment plant notified us that one of their actuator’s vibration levels spiked during a weekly test. Our team reviewed the data, and the pattern matched what we see with a worn yoke pin. We scheduled a minor maintenance shutdown two weeks later to replace the pin, avoiding a failure that would have cut off water supply to the plant’s main tank. Without vibration monitoring, that failure would have happened during peak demand, leading to supply disruptions for the entire city district.
Temperature sensors round out the core monitoring suite, and they serve two critical purposes: protecting the actuator itself and ensuring process safety. Scotch Yoke actuators rely on lubrication for all moving parts—if bearings or gears run too hot, the lubricant breaks down, leading to increased friction, wear, and eventual seizure. We recommend installing thermocouples or resistance temperature detectors (RTDs) on three key points: the main bearings, the gear housing, and the connecting rod pin. These sensors can alert operators if temperature rises above the manufacturer’s recommended limit (usually around 180°F for standard lubricants, or higher for synthetic oils). For actuators installed in high-temperature process areas, like adjacent to a furnace, we also suggest adding ambient temperature sensors near the actuator, as extreme heat can degrade internal components even if the actuator isn’t moving. Temperature monitoring also ties into process safety: if the actuator’s internal temperature spikes unexpectedly, it could mean the valve is stuck open or closed, leading to overpressure in the line. A chemical plant we partner with uses their actuator temperature data to trigger an immediate valve shutoff if temperatures rise 20°F above baseline. Last quarter, a faulty air line caused the actuator for a reactor inlet valve to seize, and the temperature sensor alerted operators within 10 seconds—preventing a reactor overpressure event that could have caused a release of hazardous material. That’s the kind of safety value that sensors deliver beyond just equipment maintenance.
Now, for the less common but highly useful sensors that many facilities overlook. First, pressure sensors for pneumatic or hydraulic actuators. Most Scotch Yoke actuators are pneumatic or hydraulic, meaning they use compressed air or fluid to generate force. Monitoring supply pressure can reveal leaks, failed regulators, or inadequate air delivery that causes the actuator to move slowly or not at all. For example, if the supply pressure drops from 80 psi to 60 psi, that could mean a leak in the air line, which would reduce the actuator’s output force and leave the valve partially open. We recommend installing pressure sensors at both the supply inlet and the point where the pressure enters the actuator’s cylinders, so you can catch leaks between the main line and the actuator itself. Another underused sensor is humidity, especially for actuators installed in outdoor or marine environments. Moisture can corrode internal parts, especially if the actuator is exposed to rain, salt spray, or high humidity. A humidity sensor paired with a temperature sensor can trigger a heater in the actuator enclosure if moisture levels rise, preventing corrosion that would otherwise lead to premature failure.
One thing I always emphasize when talking with customers: data is only useful if you act on it. Too many facilities collect sensor data and store it in a system that no one reviews, or set alarm thresholds so high that alerts come too late. As a Scotch Yoke actuator supplier, we don’t just sell you the sensors and the actuators—we help you integrate the data into your existing maintenance management system (CMMS), set smart, custom thresholds, and even offer predictive analytics tools that use the sensor data to recommend maintenance before a failure happens. For example, our remote monitoring platform can analyze vibration, force, and position data to predict when a yoke pin will wear out, so you can schedule the replacement during a planned shutdown instead of reacting to an unplanned outage.
I’ve seen first-hand how investing in the right sensors pays off for our customers. The total cost of installing four core sensors (position, load, vibration, temperature) on a Scotch Yoke actuator is usually less than 5% of the actuator’s total cost, and the return on investment is measurable: unplanned downtime drops by up to 70%, maintenance costs are reduced by 30-40%, and actuator lifespan is extended by 2-3 years. That’s not just a number—it’s our customers saving millions of dollars annually in lost production and repair costs.
If you’re operating Scotch Yoke actuators in your facility and want to learn more about which sensors are right for your specific application, or how to integrate monitoring into your existing setup, we’re here to help. We work with plants of all sizes, from small local processing facilities to large multinational energy companies, to design customized monitoring solutions that fit their needs and budget. Whether you’re looking to retrofit existing actuators or equip new ones, our team has the expertise to guide you every step of the way. Reach out to our sales team to discuss your requirements and get a tailored recommendation for your Scotch Yoke actuator monitoring needs.
Pneumatic Rotary Actuator References:
- Scotch Yoke Actuator Design and Application Guide. International Society of Automation, 2021.
- Vibration Monitoring for Reciprocating Industrial Equipment. Machinery Reliability Association, 2020.
- Load and Force Monitoring for Valve Actuation Systems. American Society of Mechanical Engineers, 2019.
- Process Safety Management for Rotating and Reciprocating Equipment. OSHA Technical Manual, 2022.
Zhejiang Bigtork Valve Automation Co., Ltd.
Zhejiang Bigtork Valve Automation Co., Ltd. is one of the leading scotch yoke actuator manufacturers and suppliers in China. We warmly welcome you to buy customized scotch yoke actuator at competitive price from our factory. Contact us for more details.
Address: 98 Yuanqu Avenue,Anfeng Industrial Zone,Oubei,Yongjia,Zhejiang,China.
E-mail: sales@bigtork.com
WebSite: https://www.bigtork.com/
